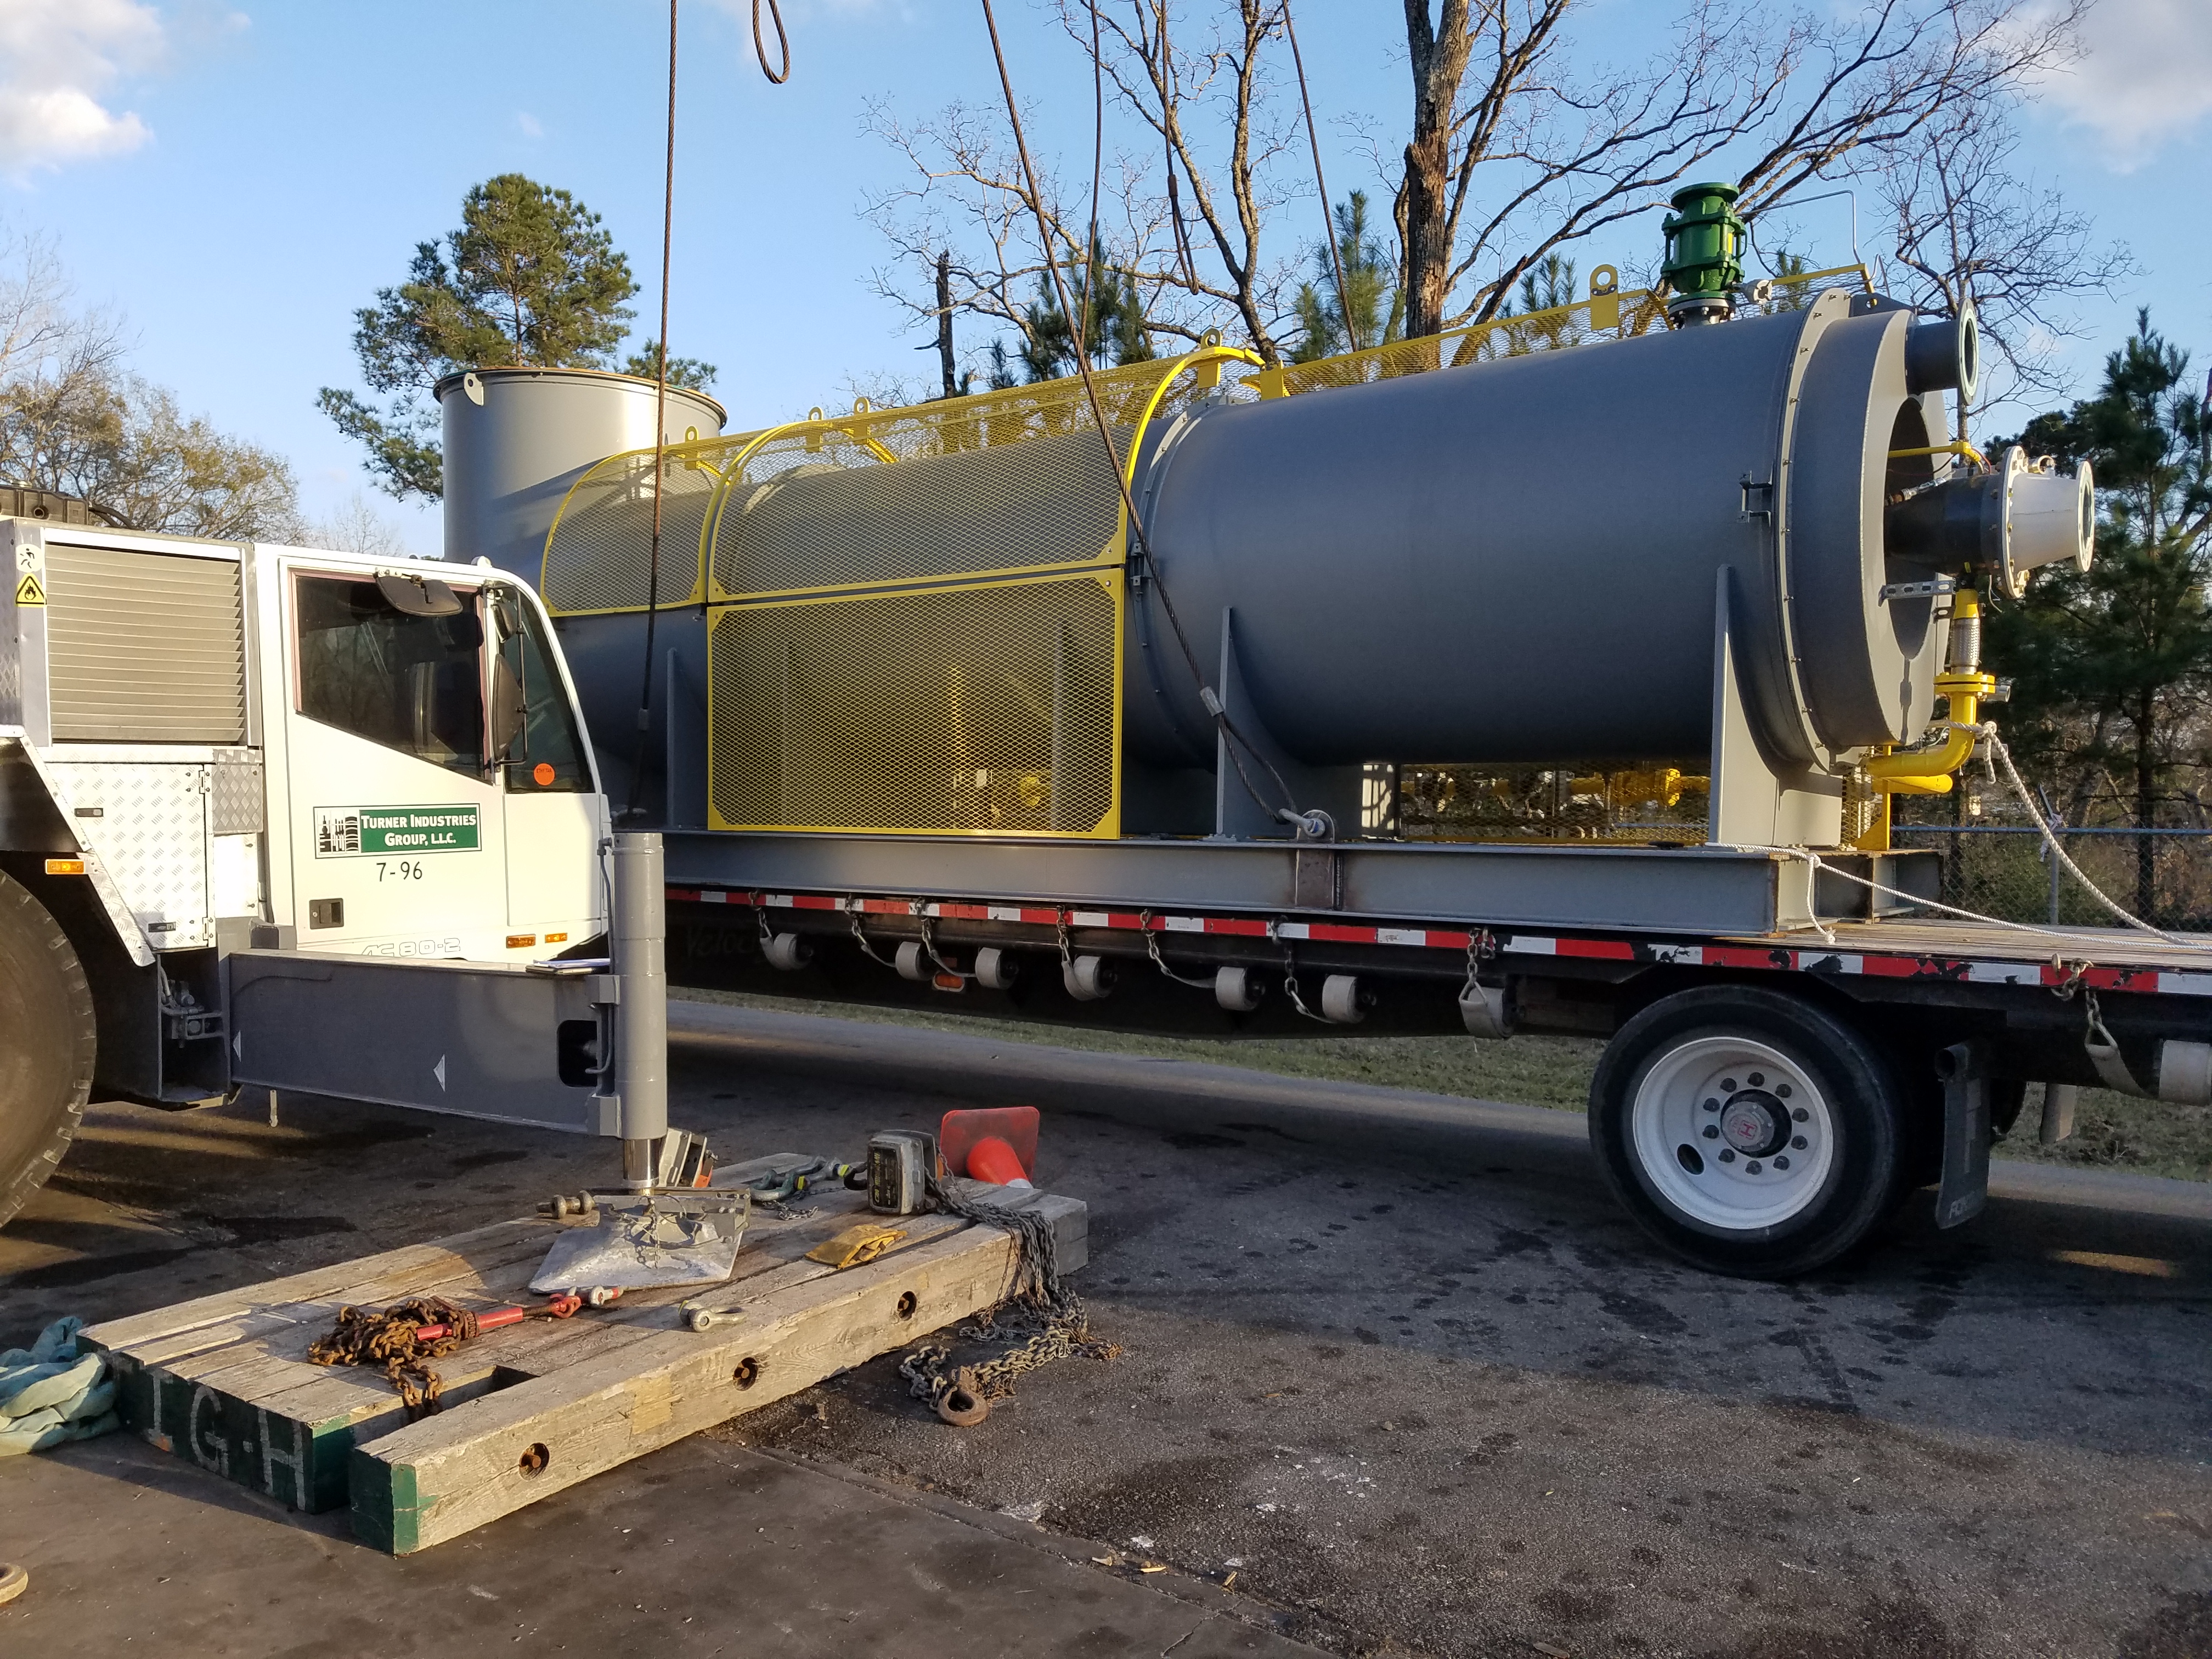
Thermal Oxidizer Retrofit & Rapid Deployment
WR Grace needed a mothballed oxidizer fully refurbished and operational in 30 days. CleanCap delivered complete modernization including Hastelloy quench tower, new PLC controls, burner system, and Class 1 Div 2 hazardous area compliance.
30 Days
Deployment Time
Compliant
Class 1 Div 2
Turnkey
System Status
Project At A Glance
Challenge
30-Day Deployment Window
Methodology
Intensive engineering review with parallel mechanical and electrical execution.
Outcome
- Deployment Time: 30 Days
- Class 1 Div 2: Compliant
- System Status: Turnkey
Executive Summary
WR Grace required a Thermal Oxidizer (TO) system to be fully refurbished, modernized, and integrated into their process within a compressed 30-day deployment window. The project included upgrading a mothballed oxidizer, adding a quench tower, installing new controls, and ensuring Class 1 Div 2 compliance. CleanCap executed a turnkey modernization that delivered rapid installation, full refurbishment, and safe operation in a hazardous environment.
Customer Background
WR Grace is a leading global producer of catalysts and specialty chemicals. Their production processes involve high temperatures, reactive chemicals, and organic vapors requiring thermal destruction. The facility needed a TO capable of destroying high-VOC off-gases while operating dependably in a hazardous area.
Project Background
The project involved a used TO vessel, an incomplete control panel, and uninstalled valves. It required engineering validation, mechanical reconstruction, electrical installation in a hazardous area, and commissioning. This was a full lifecycle modernization executed under extreme time pressure.
The CLEAN Approach
Consult & Analyze
- Mechanical Assessment: The vessel required refractory patching and significant cleaning.
- Controls Assessment: Existing controls were outdated and non-compliant with Class 1 Div 2.
- Process Review: Analyzed VOC loading and integration requirements with boiler/scrubber.
- Root Cause: This was a reconstruction requiring engineering completion, not just assembly.
Learn & Plan
- Control Modernization: Designed new PLC/HMI system with safety interlocks.
- Quench Tower Integration: Configured Hastelloy tower to protect downstream equipment.
- Valve Upgrade: Engineered specs for MODBUS flow meters and pneumatic actuators.
- Schedule: Created a minute-by-minute execution plan to meet the 30-day deadline.
Execute with Precision
- Mechanical Reconstruction: Restored structural components and repaired refractory.
- Quench Tower: Installed tower and connected cooling lines.
- Controls: Built new control panel with hazardous-rated wiring.
- Startup: Performed dry run, safety checks, and calibrated destruction efficiency.
Assess & Document
- Performance Validation: Achieved temperature stability and destruction efficiency.
- Quench Performance: Reduced exhaust temperature to target levels.
- Documentation: Provided as-built drawings, P&IDs, and operations manual.
Nurture & Maintain
- Established support program including operator training, scheduled burner tuning, and quarterly health inspections.
Results & Impact
Operational Results
- Successful commissioning under extreme time constraints
- Fully modernized system
- Improved process stability
Compliance & Safety
- Reliable VOC destruction
- Full Class 1 Div 2 compliance
- Improved operator safety
"CleanCap turned a fragmented, non-operational oxidizer into a fully engineered, production-ready emissions control system in record time."